Water is an essential resource in manufacturing industries. It is used for production, equipment cleaning, cooling and various processing activities. However, raw water from borewells, rivers and other sources may contain dissolved salts, excess minerals, iron and suspended impurities. Using untreated water can affect product quality, damage equipment and increase maintenance costs.
An Industrial Reverse Osmosis (RO) Plant helps overcome these challenges by reducing dissolved salts and unwanted impurities, providing treated water suitable for different industrial applications.
Why Do Manufacturing Industries Need Industrial RO Plants?
Water quality requirements vary depending on the manufacturing process. Textile industries need suitable water for dyeing, while food processing and pharmaceutical units require water that meets specific quality standards.
High TDS, hardness and other impurities can cause scaling, deposits and operational problems. An industrial RO plant helps improve water quality and supports consistent manufacturing operations.
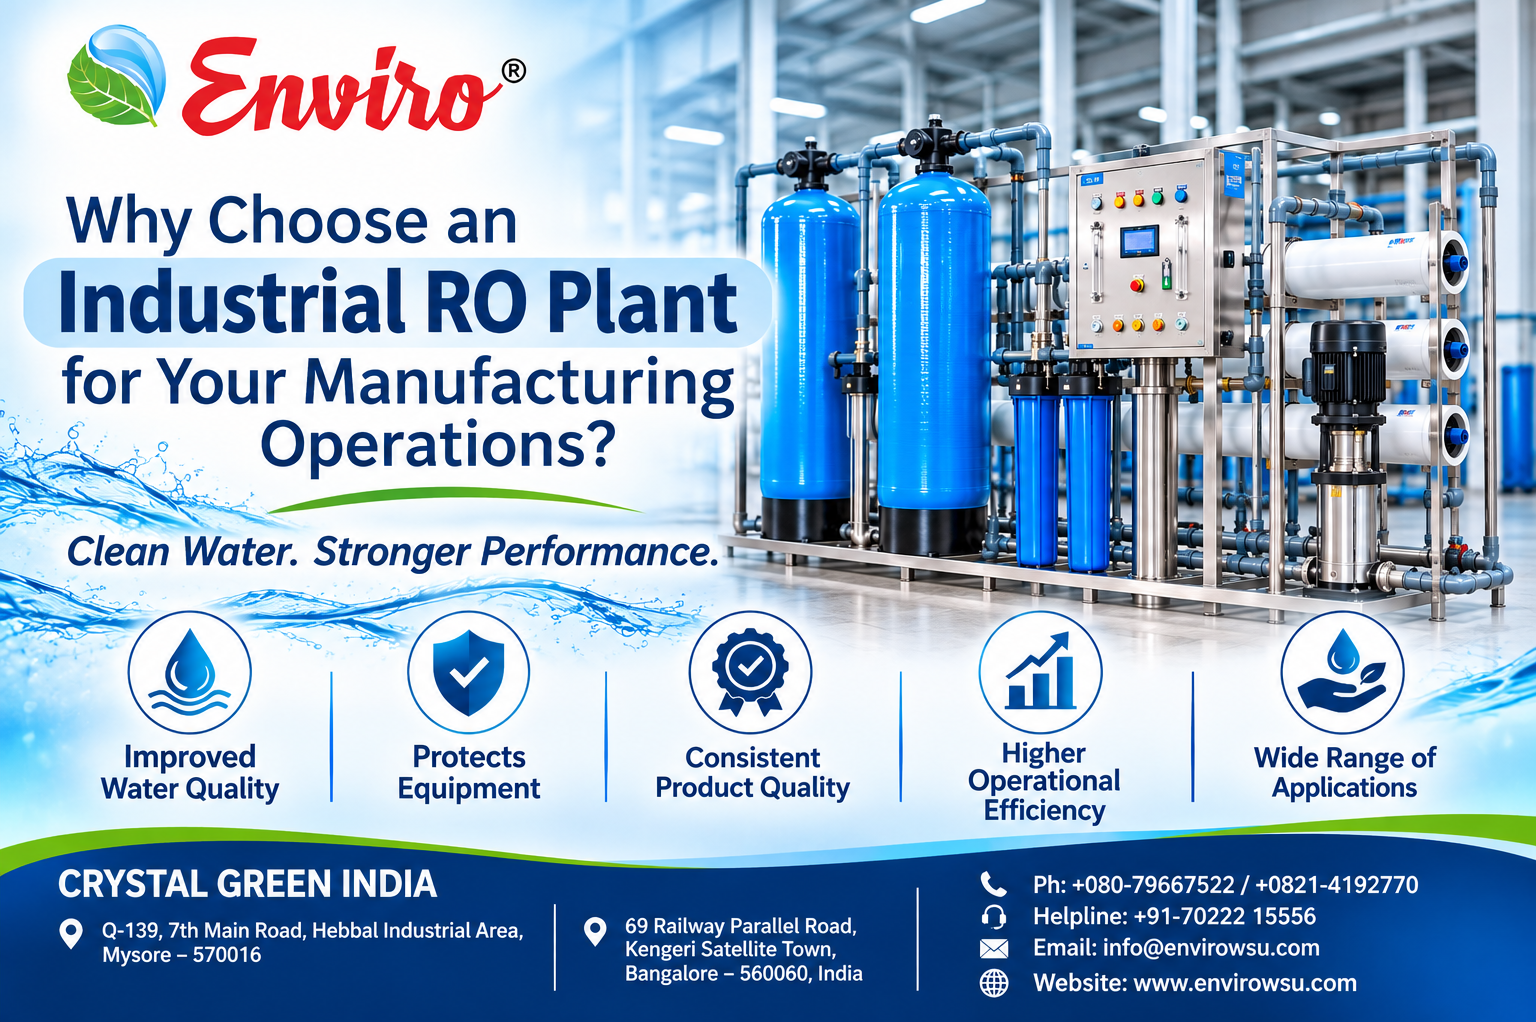
Key Benefits of Industrial RO Plants
1. Improved Water Quality
Industrial RO plants reduce dissolved salts and several unwanted impurities in raw water. This helps maintain consistent water quality for manufacturing processes where water purity is important.
2. Protection of Industrial Equipment
Excess hardness and dissolved minerals can cause scale deposits in pipelines, boilers and heat exchangers. Proper water treatment helps minimise these problems, supporting equipment performance and reducing maintenance requirements.
3. Consistent Product Quality
Water quality can influence products manufactured in textile, food processing, pharmaceutical and chemical industries. An appropriately designed RO plant provides more consistent treated water, supporting reliable production standards.
4. Reduced Dependence on External Water Suppliers
An in-house RO plant allows manufacturing units to produce treated water according to their daily requirements, reducing dependence on purchased purified water and providing better control over water availability.
5. Multiple Industrial Applications
Industrial RO plants can be customised for:
• Food and beverage processing
• Pharmaceutical manufacturing
• Textile processing and dyeing
• Chemical and automobile industries
• Boiler feed-water pretreatment
• Cooling tower makeup water
• Industrial cleaning and washing
6. Better Operational Efficiency
A properly designed RO system with suitable pretreatment and regular maintenance helps maintain stable water production and reduces issues associated with poor-quality raw water.
Main Components of an Industrial RO Plant
An industrial RO plant consists of different filtration and purification stages:
• Pressure Sand Filter (PSF): Reduces suspended particles and turbidity.
• Activated Carbon Filter (ACF): Helps remove free chlorine, organic impurities and unwanted odour.
• Micron Cartridge Filter: Removes fine particles before water enters the RO membrane.
• High-Pressure Pump: Provides the pressure required for reverse osmosis.
• RO Membrane: Separates a significant portion of dissolved salts and impurities.
• Control Panel: Helps monitor and control plant operation.
The system configuration depends on raw water quality, required capacity and the intended application.
How to Choose the Right Industrial RO Plant?
Before installation, manufacturing industries should consider a few important factors:
1. Raw Water Analysis: Check TDS, hardness, iron, turbidity and other water quality parameters.
2. Required Capacity: Calculate daily water consumption and production requirements.
3. Application: Identify the treated-water quality needed for the manufacturing process.
4. Pretreatment: Select suitable filtration stages to protect the RO membrane.
5. Maintenance: Plan regular servicing, membrane cleaning and filter replacement.
Choosing a system based on actual water conditions and industrial requirements helps achieve reliable performance and better long-term value.
Conclusion
An industrial RO plant is a valuable investment for manufacturing industries that depend on consistent water quality. It helps reduce unwanted impurities, protect equipment, maintain production quality and improve water management.
Selecting the right system with suitable pretreatment, quality components and professional installation makes a significant difference in long-term performance.
Crystal Green India provides industrial RO plants and customised water treatment solutions for manufacturing units and commercial applications.
One Brand. Complete Water Treatment Solutions.
Website: www.envirowsu.com